How to Improve Process Control with Six Sigma Tools
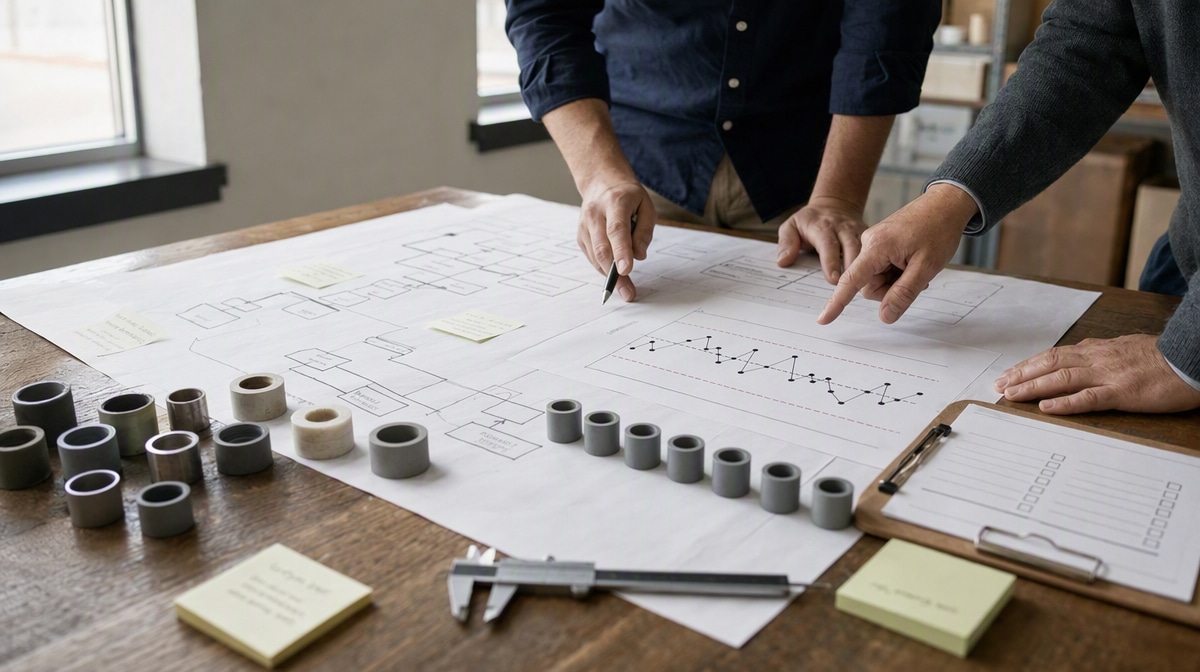
A process can look reliable at each step and still lose a meaningful share of good output by the end. This becomes costly when a business handles a high volume of transactions, depends on several connected steps, or cannot easily correct an error after it reaches a customer.
Six Sigma tools improve process control by defining the requirement, measuring variation, finding its source, testing an improvement, and monitoring the result. The effort is worth considering when variation, rework, risk, or cumulative yield loss materially affects your core business processes.
Improve Process Control with Six Sigma Tools
Aiming for perfection is a pretty lofty concept, especially when you are speaking of a complete management system. Moving toward perfection requires measurement, analysis, and documentation. If you want the closest thing to it, you need sophisticated tools, but the real question is whether driving toward perfection is worth the effort.
Process control is not the same as demanding perfection. It means knowing the required result, measuring the process consistently, separating routine variation from unusual signals, and responding before a problem becomes normal. Six Sigma provides a disciplined way to organize that work and support quality improvement.
Start with a process that matters. Define its customer requirement, select one or two meaningful measures, and establish a reliable baseline. Then use the data to locate the step or input that contributes the most variation. This keeps the project focused on a business problem instead of turning statistical analysis into an end in itself.
An organization begins with its current process capability, which may depend on tribal or basic knowledge based on first-time experiences. As systems are put in place, measurement and modeling tools can support significant process improvement. This progression may improve control, but it is not a formal sigma pyramid and does not mean an organization must apply DFSS after reaching a particular sigma level.
Six Sigma DMAIC
DMAIC is a structured approach for improving an existing process that does not consistently meet performance standards or customer expectations. The name stands for Define, Measure, Analyze, Improve, and Control. It is a method that uses problem-solving and statistical tools, not a single tool by itself.
- Define: State the problem, customer requirement, scope, and improvement goal.
- Measure: Map the current process, confirm the measurement method, and collect baseline data.
- Analyze: Test which steps, inputs, or conditions are associated with defects and variation.
- Improve: Change the process, pilot the change, and compare the result with the baseline.
- Control: Standardize the improved method, monitor the key measure, and use a reaction plan when a signal appears.
This sequence complements other stages of process improvement. If a new product or process must be designed rather than an existing one improved, Design for Six Sigma commonly uses a related path called DMADV: Define, Measure, Analyze, Design, and Verify. NIST distinguishes DMAIC for existing-process improvement from DMADV for new process or product design.
Six Sigma and Error Rate
A sigma is a standard-deviation unit. Standard deviation describes how widely observations are dispersed around an average. It does not, by itself, predict the next result or convert directly into the percentage of products that will be scrapped. A defect estimate also depends on the specification limits, the shape and stability of the process distribution, and the number of defect opportunities in each unit.
That distinction matters because Six Sigma references often express performance as defects per million opportunities, or DPMO. An opportunity is not necessarily a finished part. A single transaction or product may contain several opportunities for a defect. For this reason, a DPMO figure should not be treated automatically as the percentage of units lost or the percentage of cost wasted.
Use sigma-level conversions only after documenting the convention and assumptions. For day-to-day control, it is often more useful to track the actual defect definition, first-pass yield, cycle time, rework, and customer requirement. A related article explains common and special causes of variation.
Six Sigma Methodology
Organizations most effectively utilize Six Sigma methodology when a process problem is important enough to justify disciplined measurement. High volume is one situation. A process that is 99% effective still yields 10 million defects across one billion transactions per year. Whether that is acceptable depends on the consequence, recovery cost, customer promise, and regulatory or safety risk.
Another situation is a critical process with multiple dependent steps. A high effective rate at every individual step can hide a much lower total effective rate for the entire sequence. Rolled Throughput Yield makes that cumulative effect visible and helps an organization avoid treating step-level quality as total process quality.
Rolled Throughput Yield
For a simple serial process, Rolled Throughput Yield is calculated by multiplying the yield of each process step. Consider a hypothetical five-step flow in which Supplier, Purchasing, Warehouse, Manufacturing, and Shipping each have a 95% first-pass yield.
| Completed steps | Calculation | Cumulative yield |
|---|---|---|
| Supplier | 0.95 | 95.00% |
| Purchasing | 0.95 × 0.95 | 90.25% |
| Warehouse | 0.95 × 0.95 × 0.95 | 85.74% |
| Manufacturing | 0.95 × 0.95 × 0.95 × 0.95 | 81.45% |
| Shipping | 0.95 × 0.95 × 0.95 × 0.95 × 0.95 | 77.38% |
The final Rolled Throughput Yield is about 77.4%, so the cumulative probability of at least one failure is about 22.6% under this simplified model. Rework loops, parallel paths, dependent failures, and multiple defect opportunities can require a more detailed calculation. The useful lesson is that step-level performance must be evaluated as a system.
Use the calculation to decide where to investigate. Compare first-pass yield at each step, examine defect types, and look for shifts in the mean or variation. This shows whether one step dominates the loss or several smaller losses accumulate across the process.
Organizations can also determine current performance by calculating the mean and variance for a process and comparing the data with requirements. This is not effectively reversing the typical process of Six Sigma. It is part of Measure and Analyze. If your calculation tells you that an area is unstable or incapable, look at the data more carefully and determine which step is having problems or whether many steps are causing a cumulative increase in error rate.
Mean, Variation, and Control Charts
NIST describes a stable process as one with a constant mean, constant variance, and constant distribution over time. Stability should be assessed before making a process-capability claim. Capability then compares the output of a stable process with its specification limits.
A control chart can help a team distinguish routine fluctuation from a signal that deserves investigation. A variables control chart uses a center line and statistically derived upper and lower control limits to monitor process behavior. Those control limits describe expected process behavior and are not the same as customer specification limits.
The chart does not correct the process on its own. Pair it with a reaction plan that states who reviews the signal, what evidence is checked, when work is contained, and how the cause and corrective action are recorded. See the Bizmanualz guide to continuous-improvement control charts.
Strong Processes and Procedures
Improvement is difficult to sustain when the best method remains tribal knowledge. Strong processes and procedures turn a successful trial into repeatable work. They define the required sequence, the measure that matters, the owner, the record to keep, and the response when the result moves outside the agreed trigger. Without strong processes and procedures, desired changes can fade and the system can return to its earlier variability.
A practical control plan can be short. The purpose is to make the improved process observable and actionable, not to create paperwork for its own sake.
| Control-plan field | Question to answer |
|---|---|
| Critical requirement | What result must the process deliver? |
| Metric and data source | What will be measured, and where will the data come from? |
| Limit or trigger | What signal requires investigation or containment? |
| Owner and cadence | Who reviews the measure, and how often? |
| Reaction plan | What happens when the trigger is reached? |
| Procedure and record | Where is the standard method documented, and what evidence is retained? |
Policies and Procedures Systems
Remember, though, a system of policies and procedures supports the Control phase only when it reflects the actual improved method. Link the procedure to the measure, responsible role, review frequency, escalation path, and change-control record. This makes it easier to train employees, audit the process, and identify when performance starts to drift.
Six Sigma does not replace operational judgment. It gives you a disciplined way to decide whether a problem is large enough to investigate, which part of the process deserves attention, whether a change improved the result, and how to keep the gain. When the measures and the procedure tell the same story, reducing variability and moving toward higher quality become part of daily management rather than a one-time project. The desired results are a capable process that meets requirements, minimizes wasted resources, and remains under the system’s control.
Frequently Asked Questions
What is the first Six Sigma tool to use for process control?
Start with a clear problem statement, a simple process map, and a reliable baseline measure. The right statistical tool depends on the data and the question, so measurement comes before a complicated analysis.
What is the difference between step yield and Rolled Throughput Yield?
Step yield measures performance at one step. Rolled Throughput Yield multiplies the yields of connected steps to estimate the probability that work passes through the complete serial process without a failure.
Are control limits the same as specification limits?
No. Control limits are calculated from process behavior and help identify unusual signals. Specification limits describe what the customer, design, contract, or regulation requires.
When is Six Sigma worth the effort for a smaller business?
It is most useful when a recurring problem has measurable consequences, enough observations exist to establish a baseline, and the team can change and monitor the process. A smaller problem may need a simpler root-cause review instead of a full project.
What belongs in a Six Sigma control plan?
Document the critical requirement, metric, data source, review cadence, owner, limit or trigger, reaction plan, standard procedure, and retained record. Keep the plan specific enough that another trained employee can act on it.