What is Meant by Variation in Processes?
Process results rarely repeat with perfect consistency. The practical question is not whether variation exists, but whether the process variability comes from the system itself or from an unusual event. Confusing those causes can lead a manager to adjust a stable process unnecessarily or ignore a real signal that the process is out of control.
When business processes operate within established limits and show a predictable pattern, they are considered in control. Wide variability, inconsistent results, or a meaningful nonrandom signal calls for investigation. Understanding what is meant by variation in processes is the first step toward choosing the right response.
What Is Process Variation?
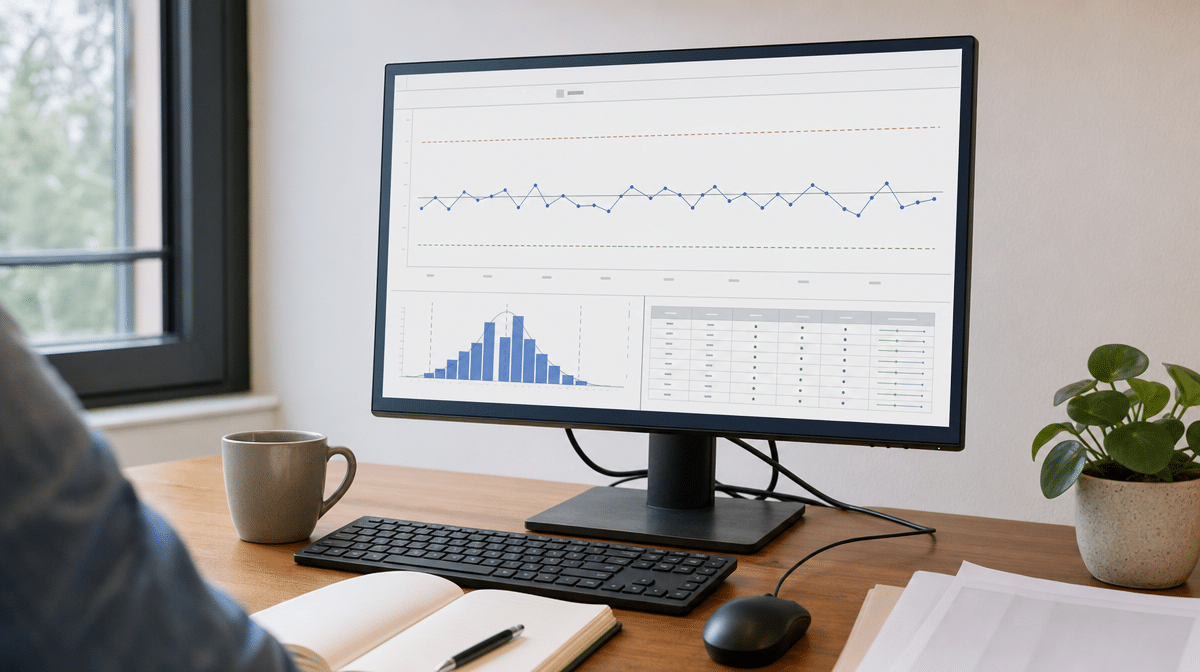
Process variation is the difference among the individual outputs of a process. Those differences may appear in cycle time, cost, dimensions, error rates, service levels, or another measured result. Every process has variation to some extent, so improvement begins by deciding whether the observed pattern is controlled variation produced by the current system or uncontrolled variation associated with a new condition.
A stable process can still produce a wide spread of results, and a narrow spread can still hide an important shift. Control limits, runs, trends, and other patterns help separate expected fluctuation from evidence that something changed. The NIST Engineering Statistics glossary describes common causes as natural sources that affect process output and explains that variation beyond a control limit can indicate a special cause.
What Are the Two Types of Process Variation?
We attribute process variability to two types of causes: common cause variation and special cause variation. The distinction matters because the type of variation determines the action. Common causes call for changes to the system, while special causes call for investigation of the unusual condition.
Common Cause Variation
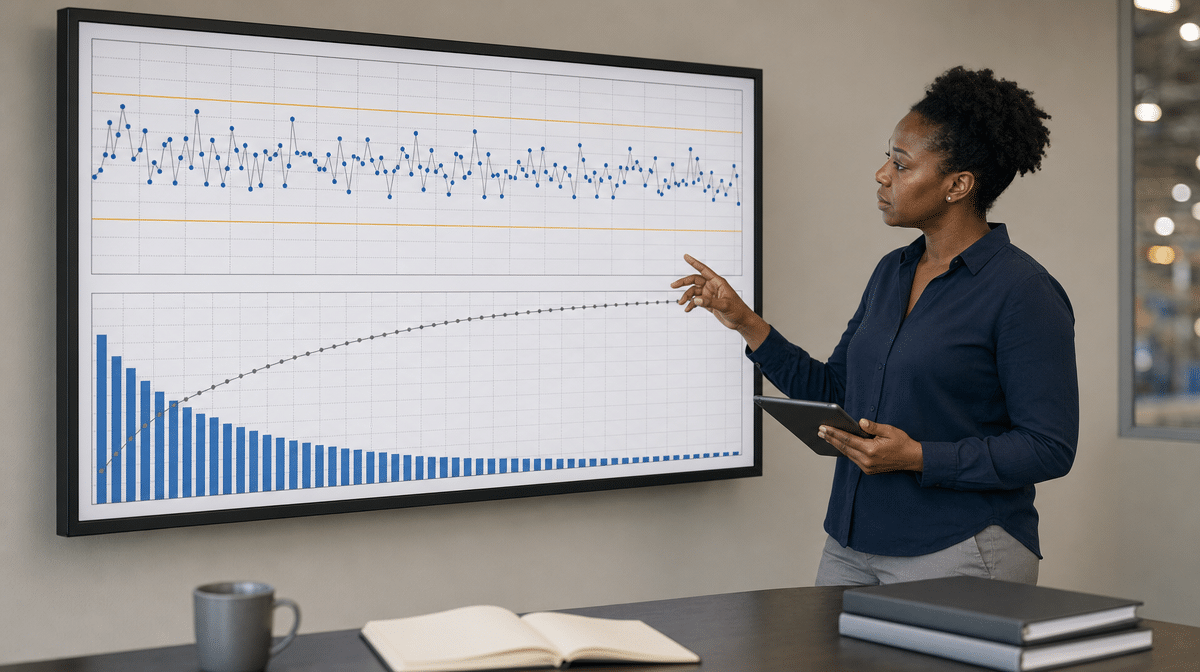
Common cause variation is expected variation generated by the process design, machinery, methods, materials, environment, and routine activities. It is always present in a stable process. Common cause variation does not have to follow a normal probability distribution, and it cannot be removed by correcting one employee or one isolated event. Correcting common cause variation means changing the system that produces the results.
Consider a person who walks to the train station every day after work. The trip usually takes six to 10 minutes. The variation is due to factors like how long the person has to wait for the elevator, how many elevator stops occur, and how long the wait is at crosswalk lights. These variations occur every day, and they are expected common cause variations.
To reduce common cause variation, the process owner usually needs experimentation and statistical analysis. Experimentation means changing something and measuring the results over time. Statistical analysis means looking at results in different ways, including stratifying and categorizing data, comparing diverse groups, and employing varying statistical methods such as Pareto charts.
In the train-station example, the person might experiment and collect data. Leaving at 4:45 instead of 5:00 could show that the elevators are less busy and that variation in the time required to reach the station is reduced. That measured change addresses a factor in the system rather than reacting to one unusual walk.
The same logic applies to a business process. Suppose invoice approval normally takes between two and four days because requests enter at different times, managers carry different workloads, and supporting documents require routine checks. Repeated reminders to one approver will not remove that common cause variation. A redesigned routing rule, a clearer document checklist, or a balanced approval queue can change the system and reduce the normal spread.
Special Cause Variation
Special cause variation is unexpected variation associated with an unusual, nonroutine, or assignable cause that is not an inherent part of the current process. The event may occur unpredictably, but it creates a signal that deserves attention. Statistical process control (SPC) can detect that signal, while a failure mode and effects analysis (FMEA) can anticipate failure risks and a control plan can define monitoring and reaction steps.
Return to the daily walk. One day, it takes 12 minutes to walk to the train station because someone approaches on the sidewalk and asks for directions. The person is lost, so the walker spends a few minutes explaining where they are and how to get where they are going, plus exchanging a few pleasantries. That does not happen very often. In fact, it hardly ever happens.
The next day, the walk returns to the six-to-10-minute window. The encounter was a special cause of variation, not a permanent change to the elevator, crosswalk, or walking process. Changing the normal departure time because of that single event would not prevent a stranger from asking for directions.
Special cause variation is typically investigated using root cause analysis. The cause in this example is easy to identify, but the cause of unexpected variation is frequently harder to see. Quality tools such as the 5 Whys and fishbone charts can help explain what happened after a control-chart signal appears.
Once the cause is understood, the process owner can eliminate it, reduce the chance of recurrence, improve detection, or consciously accept it. A rare event may simply be ignored when it happens rarely and the consequences are acceptable. Helping a lost person and missing a train may be an acceptable outcome; a rare machine fault that creates a safety hazard is not.
In the invoice process, a system outage that holds one batch for nine days is a special cause. The correct response is to investigate the outage, restore service, recover the affected invoices, and decide whether a backup or alert is justified. Redesigning the entire approval queue before confirming the outage would mix a local corrective action with a system-improvement decision.
How Does SPC Improve a Process?
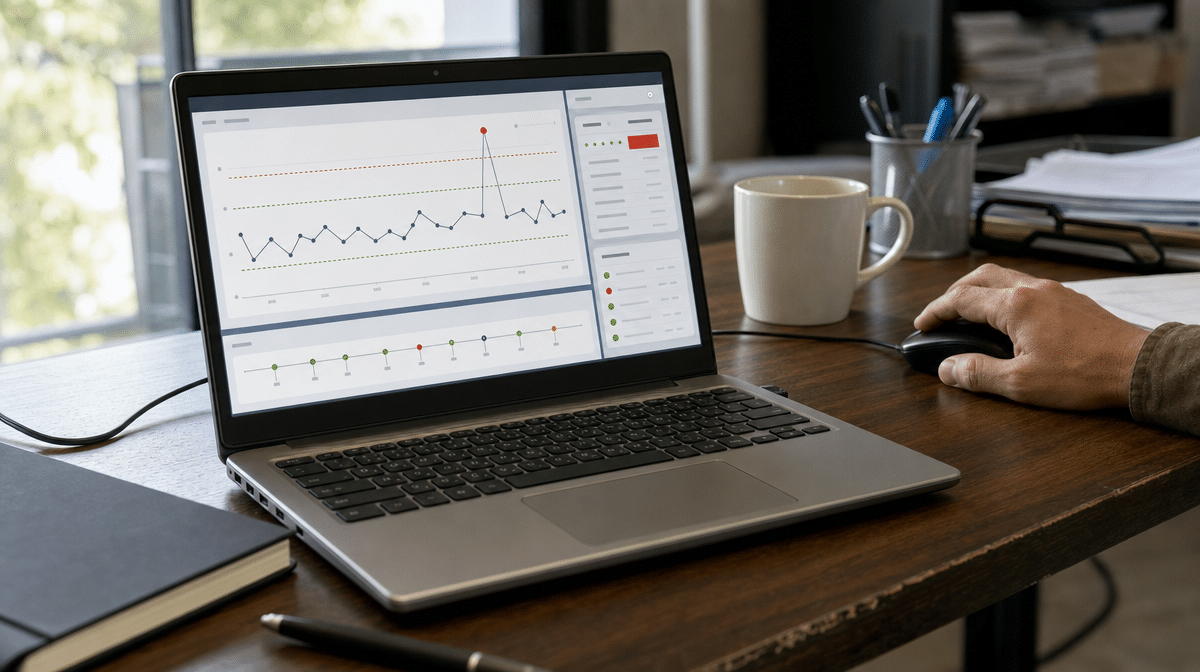
SPC process improvement uses data collected in time order to distinguish a stable pattern from evidence of change. A control chart includes a center line and calculated upper and lower control limits. The NIST control-chart guidance explains how these limits support decisions about whether a process is operating in statistical control.
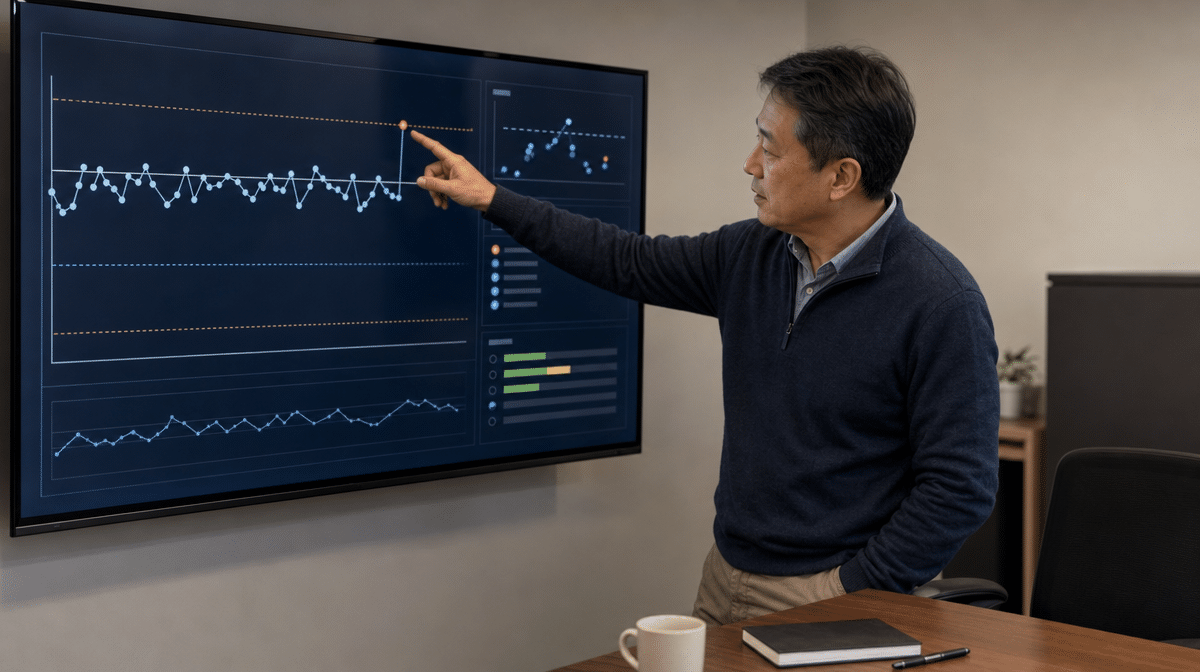
A point outside a control limit is one signal, but it is not the only signal. A sustained run on one side of the center line, a trend, a cycle, or another nonrandom pattern can also indicate a special cause. Teams should use an appropriate chart for the data and document what they investigated, what they learned, and what action followed.
Useful analysis depends on a consistent operational definition. Decide what counts as a completed cycle, defect, delay, or exception before collecting data. Record the result in time order and capture relevant context such as shift, machine, supplier, product type, location, or approver. Those categories support stratifying and categorizing data without changing the chart rules after a surprising result appears.
Control limits are calculated from process data; they are not the same as customer specifications or management targets. A process can be statistically stable and still fail customer requirements, which means the common-cause system needs improvement. It can also meet specifications while showing a special-cause signal that warns of an emerging problem. Stability and capability answer different questions.
1. Find and Address Special Causes
When a special cause is present, the process may be out of control. Mark the signal, investigate the time and conditions around it, identify the assignable cause, and take proportionate action. The objective is to eliminate it from occurring again when the risk and consequences justify prevention.
2. Reduce Common-Cause Variation
Common cause is always present when the process is in control. To reduce the variation, assess the system and change the process design, machinery, methods, materials, training, workload, or other recurring conditions. Local corrective action aimed at one person cannot solve a system-level source.
3. Confirm the Improved Process
An improved process results from eliminating special causes of an out-of-control process or reducing variability by changing the system of an in-control process. Continue collecting data after the change. A new stable pattern with less spread, fewer errors, or a better center confirms improvement more reliably than a single favorable result.
How Should You Respond to Process Variation?
When addressing process variability, first determine whether the variation is due to a common cause or a special cause. The type of variation determines the action. Use control charts for continuous improvement to detect patterns, then choose investigation or system redesign rather than reacting to every data point.
Six Sigma tools such as SPC help detect and quantify process variation. FMEA helps teams anticipate how a process might fail, and control plans establish what to monitor and how to react. These methods support better decisions, but they do not replace operational judgment about risk, cost, customer impact, and acceptable consequences.
The central rule is simple: do not treat a common cause as though one unusual person or event created it, and do not treat a special-cause signal as ordinary noise. Classify the cause, act at the right level, and measure the results over time.
Frequently Asked Questions
What Is Process Variation?
Process variation is the difference among individual outputs of the same process. It can appear in time, cost, dimensions, defects, service levels, or another measured result.
What Is Common Cause Variation?
Common cause variation is the expected variation produced by the current system over time. Reducing it requires a change to the process design, methods, machinery, materials, environment, or other recurring conditions.
What Is Special Cause Variation?
Special cause variation comes from an unusual, nonroutine, or assignable condition that is not inherent in the process. It should be investigated and addressed according to its risk and consequences.
How Does SPC Detect Process Variation?
SPC plots process data in time order and uses control limits plus pattern rules to distinguish stable variation from possible special-cause signals. The signal prompts investigation; it does not identify the cause by itself.
How Should You Respond to Common and Special Causes?
Improve the system to reduce common-cause variation. Investigate and address the assignable condition behind a special cause, then continue measuring to confirm that the process is stable.